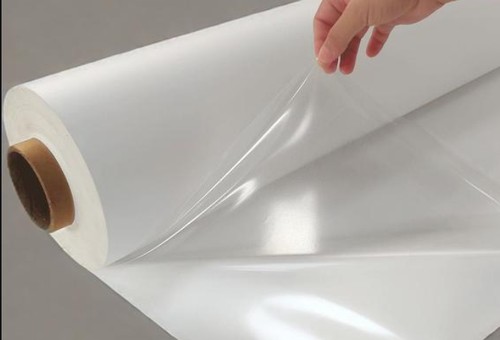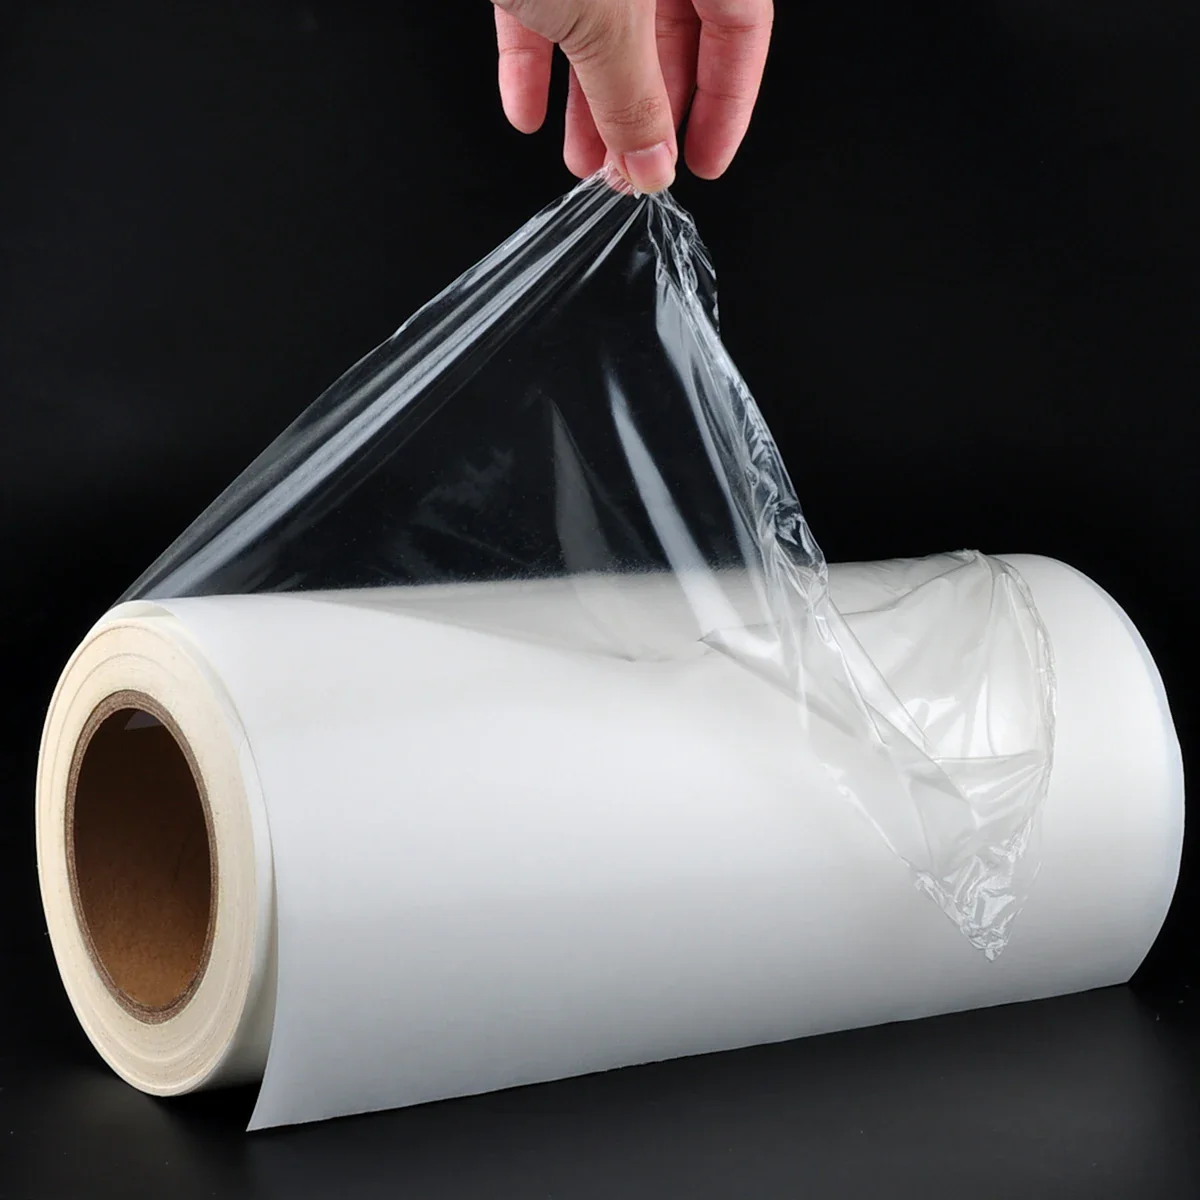

TPU laminated fabric has become a go-to material for outdoor gear, medical wearables, and performance apparel. But once you’ve bonded a TPU film to a textile, the next question almost always hits the production floor: can you actually print on it?
The short answer is yes—but the process is far less forgiving than printing on plain cotton or polyester. TPU (thermoplastic polyurethane) is a low-surface-energy, elastic, and often transparent substrate. Standard screen-printing inks and heat-transfer vinyls that work on nylon or lycra frequently fail on TPU: they crack, peel, or bleed. The difference between a durable print and a production disaster comes down to three variables: ink chemistry, surface treatment, and curing discipline.
Below is a practical breakdown based on real-world TPU film applications, including technical data from established suppliers such as Shanghai Xin Gen Tech Co., Ltd. (Xin Gen Tech) and comparable materials from major chemical and film manufacturers like Covestro, BASF, and Huntsman.
1. Understand Your TPU Surface Before You Print
Not all TPU films are the same. A matte, embossed TPU film for footwear uppers behaves very differently from a glossy, optical-grade TPU film used in bulletproof glass lamination or medical dressings.
Key data point: TPU films typically have a surface energy between 34–40 dynes/cm. For reference, solvent-based inks generally require a substrate of at least 38–42 dynes/cm for proper wetting and adhesion. That gap is why untreated TPU often rejects ink.
Case in point: In a 2023 project involving TPU film for bulletproof glass lamination in Brazil, the customer needed stable adhesion between polycarbonate and glass. The recommended solution was a high-adhesion TPU film with stable optical clarity—not a printable grade. Printing on that film would have compromised optical performance. This illustrates a critical rule: if the TPU is engineered for optical clarity or structural bonding, printing may degrade its primary function.
Practical tip:
Request the technical data sheet (TDS) for your TPU film. Look for surface energy, thickness tolerance, and whether it is designated as “printable” or “lamination grade.”
Xin Gen Tech, for example, supports customized thickness, hardness, and functional requirements. For printing applications, specify that you need a printable TPU grade with consistent surface treatment.
If you are sourcing from Covestro or BASF, their Desmopan and Elastollan TPU grades include specific print-recommended variants. Always confirm with the supplier rather than assuming.
2. Choose the Right Ink Chemistry
This is where most projects fail. There is no universal TPU ink. The choice depends on your printing method, desired stretchability, and end-use environment.
Ink types that work on TPU:
Solvent-based polyurethane inks: The industry standard for TPU. They chemically bond with the TPU surface and remain flexible. Suitable for screen printing and pad printing. However, they require proper ventilation and curing at 80–120°C.
Water-based PU inks: Growing in popularity due to lower VOC emissions. Adhesion is slightly lower than solvent-based, but modern formulations from companies like Daikin and DIC have closed the gap. Best for apparel and medical applications where solvent residue is a concern.
UV-curable inks: Fast curing, excellent for high-speed production. But UV inks can become brittle on TPU unless formulated with flexible oligomers. They work best on rigid or semi-rigid TPU, not on high-stretch films.
Silicone-based inks: Used for extreme stretch and weather resistance. Adhesion to TPU is moderate and often requires a primer. More common in technical outdoor gear.
What does NOT work well:
Standard PVC plastisol inks: They do not bond to TPU and will peel.
Conventional heat-transfer vinyl (HTV): Most HTV requires a cotton or polyester surface. On TPU, the adhesive layer often fails after a few wash cycles.
Practical tip:
Xin Gen Tech’s in-house laboratory can simulate mass production lines on a 1:1 basis, which means you can test ink adhesion on actual production-grade TPU before committing to a full run. Sample width is 400mm, and sampling lead time is fast and low-cost. This is far more reliable than testing on a generic TPU sheet from a distributor.
3. Surface Treatment Is Non-Negotiable
Even the best ink will fail on an untreated TPU surface. The low surface energy and smooth finish of TPU films mean you must mechanically or chemically modify the surface.
Proven methods:
Corona treatment: The most common inline method. It raises surface energy to 42–48 dynes/cm. Best for thin films (0.05–0.3mm). Effect diminishes over time, so print within 24–48 hours.
Plasma treatment: More uniform than corona, especially on thicker or 3D TPU parts. Atmospheric plasma systems from companies like Plasmatreat are used in automotive and medical TPU printing.
Chemical primer: A thin layer of PU primer applied before printing. Effective but adds a process step and drying time. Common in footwear and automotive interior applications.
Flame treatment: Used for thicker TPU sheets and molded parts. Less common for thin films due to risk of distortion.
Data point: In footwear and bags—currently the largest consumer market for TPU—athletic shoe cushioning and upper decoration often use TPU films laminated with fabrics for waterproof and breathable properties. When printing logos or decorative patterns on these laminates, brands like Nike and Adidas typically specify corona-treated TPU with solvent-based PU ink, followed by a heat cure at 100°C for 3–5 minutes.
Practical tip:
If you are using Xin Gen Tech’s TPU films, ask for the recommended surface treatment protocol. Their R&D center and product laboratory can advise on corona wattage, plasma settings, or primer selection based on your specific TPU grade.
4. Master the Curing and Adhesion Testing
Printing is only half the battle. Curing determines whether your print survives washing, abrasion, and flexing.
Curing guidelines for TPU:
Solvent-based PU ink: 80–120°C for 2–5 minutes. Lower temperatures require longer time.
Water-based PU ink: 120–150°C for 3–5 minutes. Must fully evaporate water before crosslinking.
UV ink: Follow the manufacturer’s UV dose. Over-curing causes brittleness; under-curing causes tackiness.
Adhesion testing you should perform:
Cross-hatch tape test (ASTM D3359): Score the print, apply tape, pull. Less than 5% removal is acceptable.
Flex test (ASTM F392): Repeatedly flex the printed TPU. Check for cracking or delamination.
Wash test: 5–10 home laundry cycles at 40°C. Check for fading, peeling, or color bleed.
Stretch test: 50–100% elongation. TPU is elastic; your ink must be too.
Case example: A European outdoor brand recently switched from a generic TPU film to a Xin Gen Tech printable TPU grade for a waterproof jacket collection. After optimizing corona treatment and switching to a water-based PU ink, they passed 10 wash cycles with no adhesion loss—a result they had not achieved with their previous supplier.
5. Consider the End-Use Before You Choose a Printing Method
TPU is used across medical, automotive, electronics, and textile industries. Each demands different print performance.
Medical: Medical-grade TPU is used in wound dressings and catheters. Printing must be biocompatible. Use water-based or solvent-free inks. Xin Gen Tech holds ISO 9001:2015, OHSAS 18001:2007, OEKO-TEX, SGS, ROHS, REACH, FDA, and EU 10/2011 certifications—critical for medical and food-contact applications.
Electronics: TPU screen protectors can self-heal minor scratches. Printing on these films requires nano-level precision and UV inks that do not interfere with optical clarity.
Automotive: TPU is used in interior parts and paint protection film. Printing must resist scratches, stone impacts, and UV fading. Solvent-based inks with clear-coat overlamination are standard.
Textiles and apparel: Composite with polyester fibers to create waterproof and breathable fabrics. Printing must survive flexing and washing. Water-based PU inks are preferred for sustainability.
Practical tip:
Xin Gen Tech appeared at the 2025 Shanghai CMEF (China International Medical Equipment Fair), showcasing innovative medical materials. If your application is medical or wearable, their team can provide samples and technical support during the sampling process to ensure your ink and TPU are compatible.
Final Thoughts
Printing on TPU laminated fabric is absolutely possible—but it is not a copy-paste process from conventional textile printing. You must:
Verify your TPU grade is printable (or accept that optical/structural grades may not be).
Select an ink chemistry matched to your stretch and durability requirements.
Apply corona, plasma, or primer treatment without exception.
Cure precisely and test adhesion with standard methods.
Work with a supplier who can provide consistent, production-grade TPU and technical support.
Companies like Shanghai Xin Gen Tech Co., Ltd. have built their reputation on exactly this kind of application support—fast sampling, stable quality, and in-house lab simulation of mass production. Whether you are prototyping a medical wearable or scaling an outdoor apparel line, the difference between a failed print and a durable one usually comes down to the five points above.
Test early, test on production-grade material, and never assume your ink will stick just because it worked on nylon. TPU is a different animal—and it rewards those who respect its chemistry.